HDPE butt fusion and electrofusion welding in Valencia
A polyethylene network is only as good as its joints. Our technicians, certified in butt fusion and electrofusion, make every weld with a controlled procedure and record it on the weld map.
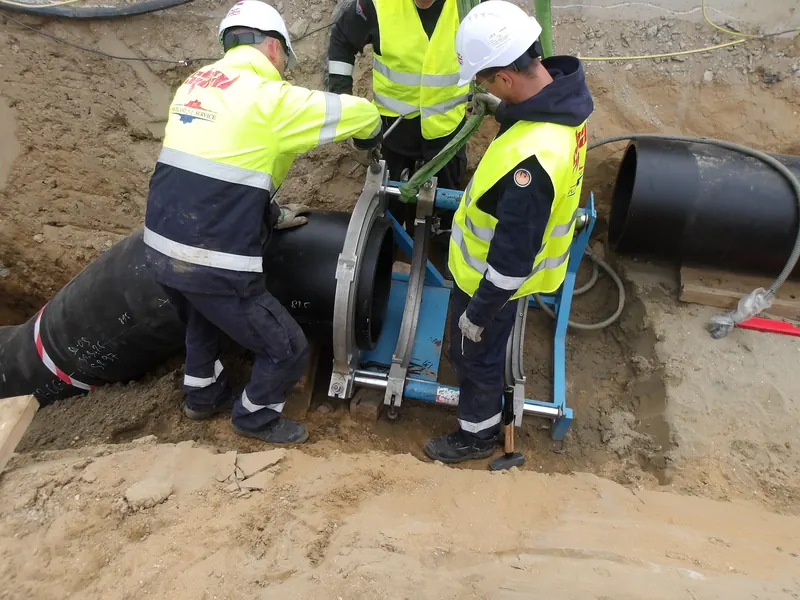
What's included
- Butt fusion welding with a heater plate
- Electrofusion of couplers, elbows, tees and tapping tees
- Welding in trenches, buildings and site workshops
- Pipe preparation, facing and alignment
- Weld map identifying every joint
- Parameter records and inspection reports
Butt fusion
The pipe ends are faced, heated with a temperature-controlled heater plate and joined under pressure until they cool. The result is a homogeneous joint with the same continuity as the pipe itself.
It is the usual method for joining pipes and fittings of the same diameter and wall thickness, especially in medium and large diameters and long runs.
Electrofusion
Fittings with a built-in heating wire are used. The electrofusion unit applies the energy defined for each fitting and fuses the surface of pipe and fitting into a single piece.
It is the right solution for repairs, tight spaces, connections to existing networks, branches and tapping tees, and joints where the pipes cannot be moved for butt fusion.
Every joint identified and recorded
Each weld is numbered on the project weld map, with its location and execution records. Together with the inspection reports and the system pressure tests, it forms part of the quality dossier we hand over at the end of the job.
Questions about butt fusion & electrofusion
When is butt fusion better, and when electrofusion?
Butt fusion is the usual choice for long runs and medium-to-large diameters with pipes of the same wall thickness. Electrofusion is used for repairs, tight spaces, connections to existing networks and branches. Many projects combine both.
How are the welds documented?
Every joint is identified on the project weld map. At handover we deliver the weld maps, inspection reports and pressure test records as part of the final quality dossier.
One contractor. The whole installation.
Send us drawings, location and timelines. We'll reply with a technical and commercial proposal.